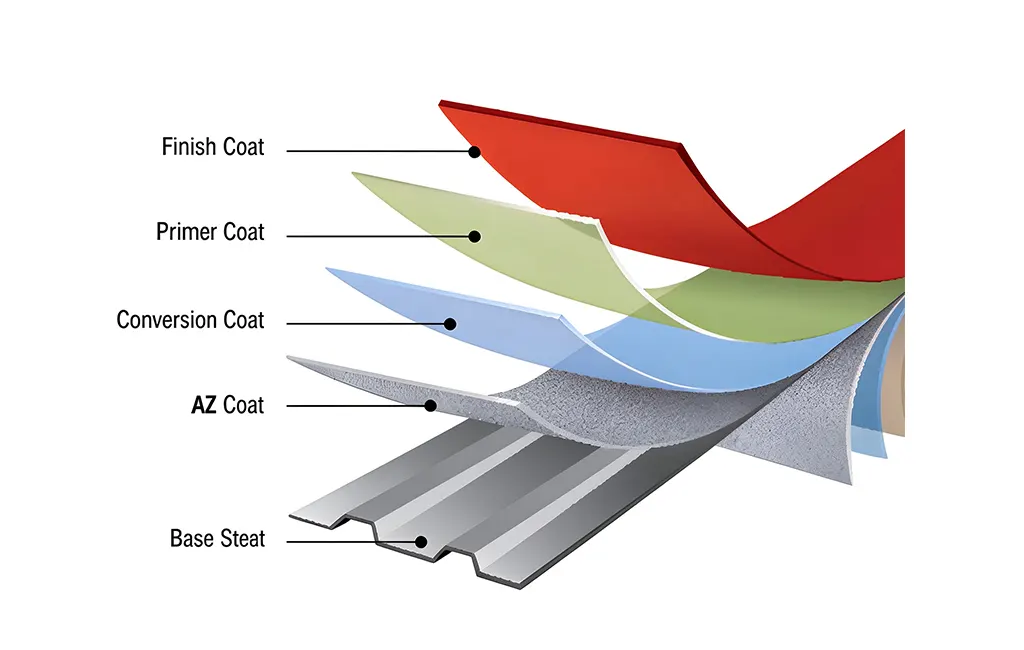
Polyethylene (PE) or polyester-based color-coated aluminum undergoes accelerated chalking in desert environments due to intense ultraviolet (UV-A and UV-B) radiation combined with extreme surface temperatures (often exceeding 70°C). Photo-oxidation breaks down the resin’s binder matrix, liberating embedded pigments as a fine white powder (chalk). Unlike Fluoropolymer (PVDF) systems, standard polyester resins lack high-energy carbon-fluorine (C-F) bonds. Exposure to high UV flux (over 200 kWh/m²/year) triggers free-radical chain reactions, degrading the polymer backbones within 2–5 years and leading to premature gloss loss and surface erosion under AAMA 2603 performance thresholds.
Coating Performance & Degradation Data Matrix
| Parameter / Specification | Standard Polyester (PE) | Super Durable Polyester (SDR) | PVDF (2-Coat System) |
| Primary Resin Base | Standard Organic Ester | Isophthalic / Neopentyl Glycol | Polyvinylidene Fluoride (70%) |
| Typical Coating Thickness | 15–20 μm | 20–25 μm | 25–30 μm |
| QUV UV-B Exposure (ASTM G154) | Fail at ~300–500 hours | 1,000–1,500 hours | > 3,000 hours |
| Florida Outdoor Test (ASTM D2244) | 1–2 Years before chalking | 3–5 Years | > 10 Years |
| Chalk Resistance (ASTM D4214) | Rating < 6 at 3 Years | Rating ≥ 8 at 5 Years | Rating ≥ 8 at 10 Years |
| Operating Temp Limit (Continuous) | 80°C | 100°C | 120°C |
| Primary Application Scenarios | Indoor panels, mild climates | Roof sheeting (mid-tier) | High-rise curtain walls, deserts |
Technical Causes of PE Coating Photodegradation
UV Radiation and Free Radical Formation
Photons in the UV spectrum (wavelengths 290–400 nm) possess energy levels (300–415 kJ/mol) that exceed the bond dissociation energy of standard ester linkages (C-O and C-C bonds ~350 kJ/mol) in polyester resins. Absorption of this energy creates radical species via Norrish Type I and Type II cleavages.
Thermal Acceleration & Sand Abrasion
Desert climates exacerbate chemical degradation through continuous thermal cycling. High ambient temperatures decrease the activation energy required for auto-oxidation, accelerating the loss of cross-linking density. Windborne sand particles act as continuous mechanical abrasives, stripping the micro-degraded top layer and exposing fresh organic resin to UV exposure.