Wood-Grain Transfer-Printed Aluminum: Technical & Application Thresholds
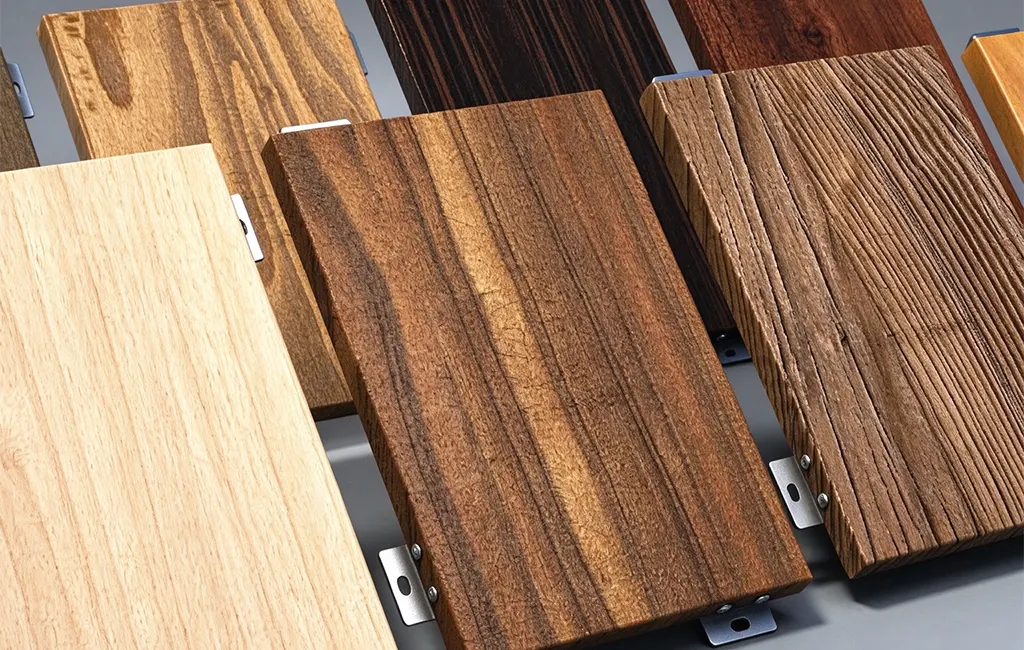
Wood-grain transfer-printed aluminum (Sublimation / Heat Transfer Film process) is selected over solid Polyvinylidene Fluoride (PVDF) color-coated aluminum when applications demand authentic biophilic aesthetics without sacrificing structural integrity, fire safety, or lightweight performance. While solid PVDF coatings rely on liquid fluoropolymer paint systems to achieve high UV resistance (AAMA 2605 compliant), heat-transfer wood-grain technology utilizes a two-step process: a powder coat base (typically polyurethane or polyester, 60–80 μm) combined with vacuum-sealed ink sublimation (15–20 μm pattern penetration). This achieves a class-A fire rating (non-combustible per ASTM E84 [1]/ EN 13501-1) and high scratch resistance, making it superior for interior feature walls, exterior soffits, screen louvers, and shaded facades where natural timber aesthetics are required but real wood presents severe rot, maintenance, and fire hazards.
Technical Specifications: Wood-Grain Transfer Aluminum vs. Solid PVDF Coated Aluminum
Evaluating wood-grain sublimation aluminum against solid PVDF coating systems requires examining substrate selection, coating composition, mechanical performance, and durability metrics under international testing protocols.
| Technical Parameter | Wood-Grain Transfer-Printed Aluminum | Solid PVDF Color-Coated Aluminum | Solid Powder-Coated Aluminum |
| Common Alloy Grades | AA6063-T5 / T6 (Extrusions), AA3003 / AA5052 (Sheets) | AA3003 / AA3004 / AA5052 (Coil/Sheet) | AA6063-T5, AA3003-H14 |
| Primary Process Tech | Base Powder Coat + Sublimation Film | 2/3-Coat Liquid PVDF Coil/Spray | Electrostatic Thermoset Powder |
| Total Film Thickness | 70–100 μm (Base: 60–80 μm; Ink: 10–20 μm) | 25–35 μm (Primer: 5–8 μm; Topcoat: 20–25 μm) | 60–90 μm |
| Color/Pattern Options | Photorealistic Wood/Marble Texture | Solid RAL Colors, Metallic, Mica | Solid RAL Colors, Textured Matte |
| Pencil Hardness | ≥ 2H (ASTM D3363) | HB – 2H (ASTM D3363) | ≥ 2H (ASTM D3363) |
| Cross-Hatch Adhesion | Class 5B / 0 Rating (ASTM D3359 / ISO 2409) | Class 5B (ASTM D3359) | Class 5B (ASTM D3359) |
| Salt Spray Resistance | > 1,000 Hours (ASTM B117 [2]) | > 3,000 Hours (ASTM B117 [2]) | > 1,500 Hours (ASTM B117 [2]) |
| QUV Accelerated Weathering | 1,500 – 3,000 Hours (ISO 16474-3 / ASTM G154) | > 4,000 Hours (ASTM G154) | 1,500 – 2,500 Hours |
| Fire Performance Rating | Class A / A2-s1, d0 (ASTM E84 [1] / EN 13501-1) | Class A / A1 Non-Combustible | Class A / A2-s1, d0 |
| Industry Standards Compliance | Qualicoat Class 1 / Class 2, AAMA 2603/2604 | AAMA 2605-20, Qualicoat Class 3 | AAMA 2604-20, ISO 12206 |
| Primary Application Scenarios | Soffits, Louvers, Ceilings, Interior Cladding, Partition Walls | High-Rise Facades, Metal Roofing, Curtain Walls | Interior Framing, Windows, Low-Rise Trim |
Decision Matrix: Wood-Grain Sublimation vs. Solid PVDF Colors
Selecting between wood-grain transfer-printed aluminum and solid PVDF color-coated aluminum involves balancing environmental exposure, fire regulations, architectural design intent, and life-cycle cost.
Choose Wood-Grain Transfer-Printed Aluminum When:
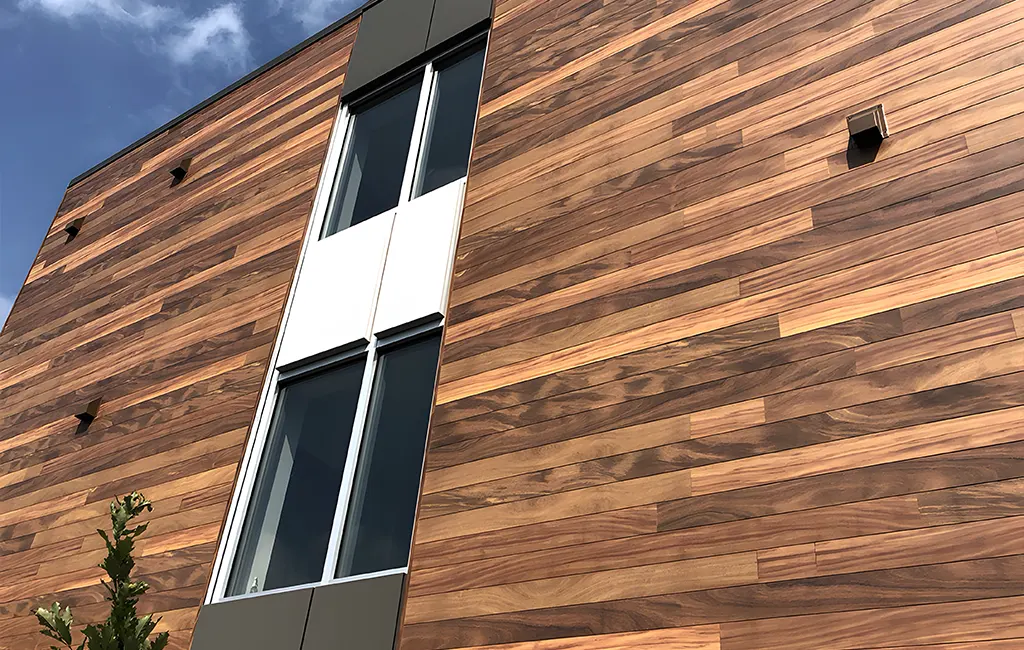
- Biophilic Design Requires Fire Compliance: Projects requiring the warmth of natural timber (e.g., airport ceilings, hotel lobbies, hospital corridors, or high-rise balconies) where local building codes ban real wood due to combustibility (ASTM E84 [1] Class A mandatory).
- High Scuff and Abrasion Resistance is Needed: Interior feature walls, doors, louvers, and column covers subject to human contact benefit from the high pencil hardness (≥ 2H) and film thickness (70–100 μm) of powder-based sublimation systems, which resist physical scratching better than softer liquid PVDF.
- Complex 3D Extrusions Are Specified: Extruded aluminum louvers, tube profiles, and intricate window framing (AA6063-T5) are better suited to powder coat base sublimation. Liquid PVDF coil coating is primarily limited to flat sheet or roll-formed applications.
- Zero Maintenance for Natural Aesthetics: Traditional wood requires periodic sanding, staining, and sealing every 2–3 years. Wood-grain aluminum provides complete resistance to rot, termites, and moisture expansion with a simple wash schedule.
Choose Solid PVDF Color-Coated Aluminum When:
- Continuous Coil-Coated Flat Panels: High-volume composite panels (ACP) or solid aluminum facade panels (AA3004 / AA5052) requiring continuous color consistency across thousands of square meters benefit from automated liquid PVDF coil coating lines.
- Extreme UV & Weather Exposure (Direct High-Rise Facades): For exterior curtain walls above 4 stories, high-altitude buildings, or equatorial zones with UV index values , 70% fluoropolymer resin (Kynar 500 [3] / Hylar 5000) solid PVDF coatings offer superior color retention ( after 10–20 years per AAMA 2605).
- Severe Marine Environments: Coastal installations within 1,000 meters of salt water require the superior chemical inertness of PVDF, which withstands > 3,000 to 5,000 hours of continuous salt spray testing (ASTM B117 [2]) compared to 1,000–1,500 hours for standard transfer-printed powder bases.
References
[1] Wikipedia. ASTM E84 [EB/OL]. 2026-09-24.
[2] Wikipedia. Salt spray test [EB/OL]. 2026-09-24.
[3] Wikipedia. Polyvinylidene fluoride [EB/OL]. 2026-09-24.