Oil Canning in Color-Coated Aluminum Panels Is Often Caused by Substrate Stress, Fabrication Conditions, and Installation Constraints
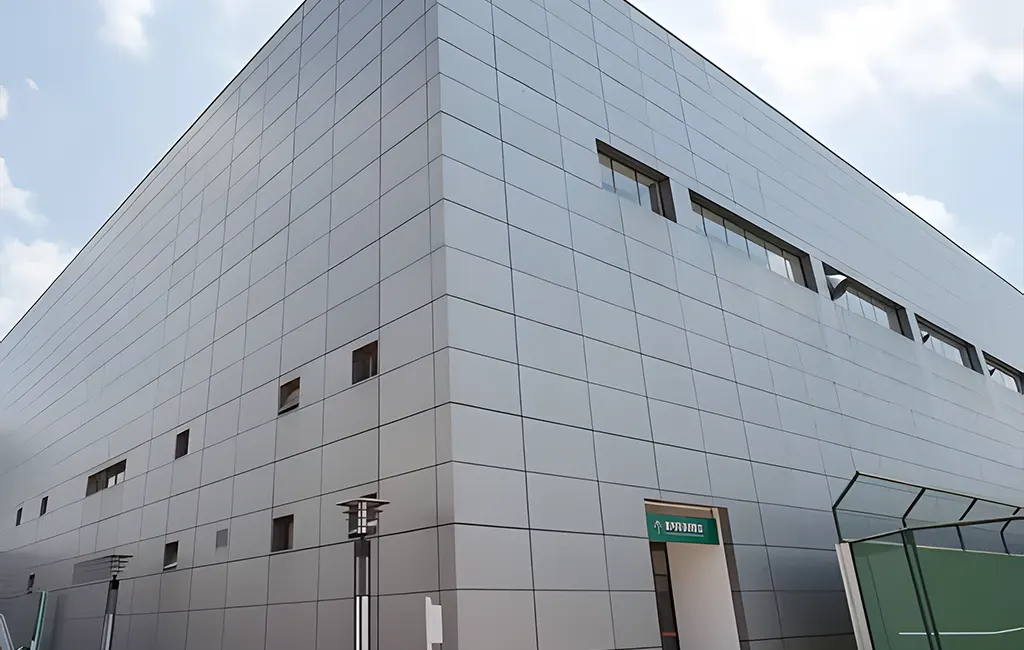
Oil canning refers to the visible waviness, buckling, or uneven surface appearance that develops on relatively flat metal panels. Color-coated aluminum panels may appear flat during factory inspection but develop noticeable deformation after installation because of residual stress, uneven substrate flatness, improper fabrication, or excessive installation restraint. Oil canning is not necessarily a coating defect; it is primarily a panel flatness and mechanical stability issue. However, the color-coated surface can make these irregularities more visible under direct sunlight and changing viewing angles. For manufacturers and buyers, controlling aluminum substrate quality, panel dimensions, support spacing, and installation methods is essential to reducing oil canning risks.
1. What Are the Main Causes of Oil Canning in Aluminum Panels?
Oil canning generally results from a combination of material characteristics and installation conditions. Even small variations in substrate flatness or residual stress can become visible when aluminum sheets are cut, formed, and fixed into large panels.
| Potential Cause | Technical Explanation | Possible Result |
|---|---|---|
| Poor substrate flatness | Uneven flatness before fabrication | Visible surface waviness |
| Residual stress | Internal stress from rolling, leveling, or fabrication | Panel distortion after cutting |
| Uneven thickness | Thickness variation across the aluminum sheet | Inconsistent forming behavior |
| Improper roll forming | Uneven forming pressure or roller adjustment | Surface buckling or deformation |
| Excessive installation restraint | Panels cannot expand or contract freely | Localized buckling |
| Incorrect support spacing | Insufficient or uneven structural support | Visible panel deflection |
| Thermal expansion | Temperature changes cause dimensional movement | Panel distortion or stress concentration |
These factors can interact. For example, a panel with residual stress may remain relatively flat before installation but develop visible waviness after being rigidly fixed to an uneven supporting structure.
2. Why Can Panels Look Flat Before Installation but Develop Oil Canning Afterwards?
One important reason is that cutting, bending, fastening, and installation can redistribute stresses within the aluminum panel.
During manufacturing, aluminum coil undergoes rolling, tension leveling, coating, and subsequent fabrication. If residual stresses remain in the material, cutting the coil into smaller sheets or forming it into panels can release or redistribute these stresses.
Installation conditions can further increase the problem:
- Fastening Pressure: Excessive screw tightening can locally deform the panel.
- Thermal Movement: Aluminum expands and contracts with temperature changes. Restricted movement can create additional stress.
- Uneven Supporting Structures: Differences in frame alignment can introduce unwanted panel deformation.
- Panel Dimensions: Large, thin panels are generally more sensitive to visible surface waviness.
- Installation Sequence: Incorrect fastening sequences can introduce uneven tension across the panel.
Therefore, factory flatness inspection alone cannot guarantee that a finished panel will remain visually flat after installation.

3. Which Aluminum Coil Parameters Influence Oil Canning?
Material selection plays an important role in controlling oil canning. Buyers should evaluate the aluminum substrate and its forming characteristics rather than focusing exclusively on the color and coating appearance.
| Technical Parameter | What to Check | Potential Influence |
|---|---|---|
| Aluminum Alloy | 3003, 5052, or other specified grade | Mechanical behavior and formability |
| Temper | O, H14, H24, or other specified condition | Strength and flexibility |
| Coil Thickness | Nominal thickness and tolerance | Panel stiffness |
| Substrate Flatness | Flatness and shape consistency | Initial surface appearance |
| Residual Stress | Material stress distribution | Distortion after cutting |
| Width and Length | Dimensional consistency | Fabrication and installation accuracy |
| Surface Quality | Scratches, dents, and coating defects | Finished panel appearance |
For example, thinner aluminum panels generally have lower bending stiffness than thicker panels of the same alloy and temper. Consequently, they may be more sensitive to support spacing, fastening pressure, and installation conditions.
However, no single alloy or temper can automatically eliminate oil canning. The final result depends on the complete combination of material properties, panel geometry, fabrication processes, and supporting structure.
4. How Can Manufacturers and Installers Reduce Oil Canning?
Reducing oil canning requires coordinated quality control throughout aluminum coil production, panel fabrication, and installation.
Manufacturers should:
- Control aluminum substrate flatness and thickness consistency.
- Maintain stable rolling and tension-leveling conditions.
- Reduce residual stress through appropriate material processing.
- Verify panel flatness after cutting and forming.
- Maintain consistent coating and fabrication processes.
Installers should:
- Ensure the supporting framework is properly aligned.
- Follow recommended panel support spacing.
- Avoid excessive fastening pressure.
- Allow for thermal expansion and contraction.
- Use appropriate fastening systems and installation sequences.
For architectural applications, trial installation of representative panels can help identify potential deformation problems before large-scale installation begins.
5. How Should Buyers Inspect Color-Coated Aluminum Panels Before Installation?
Buyers should establish clear flatness and appearance requirements before production rather than relying only on the visual inspection of the aluminum coil.
Recommended inspection procedures include:
- Incoming Material Inspection: Check aluminum thickness, width, surface condition, and substrate flatness.
- Fabrication Inspection: Examine panels after cutting, bending, and roll forming.
- Dimensional Verification: Confirm panel dimensions and forming accuracy.
- Flatness Assessment: Inspect panels on a suitable reference surface under consistent conditions.
- Trial Installation: Evaluate representative panels using the actual support and fastening system.
- Visual Inspection: Check for waviness, buckling, and uneven reflections under consistent lighting.
It is also important to distinguish oil canning from coating defects. Oil canning is characterized by visible panel waviness or distortion, whereas coating defects involve problems such as peeling, blistering, cracking, or uneven color.
References
[1] Wikipedia contributors. Aluminium [EB/OL]. 2026-03-29.
[2] Wikipedia contributors. Coil coating [EB/OL]. 2026-03-29.
[3] Wikipedia contributors. Thermal expansion [EB/OL]. 2026-03-29.