
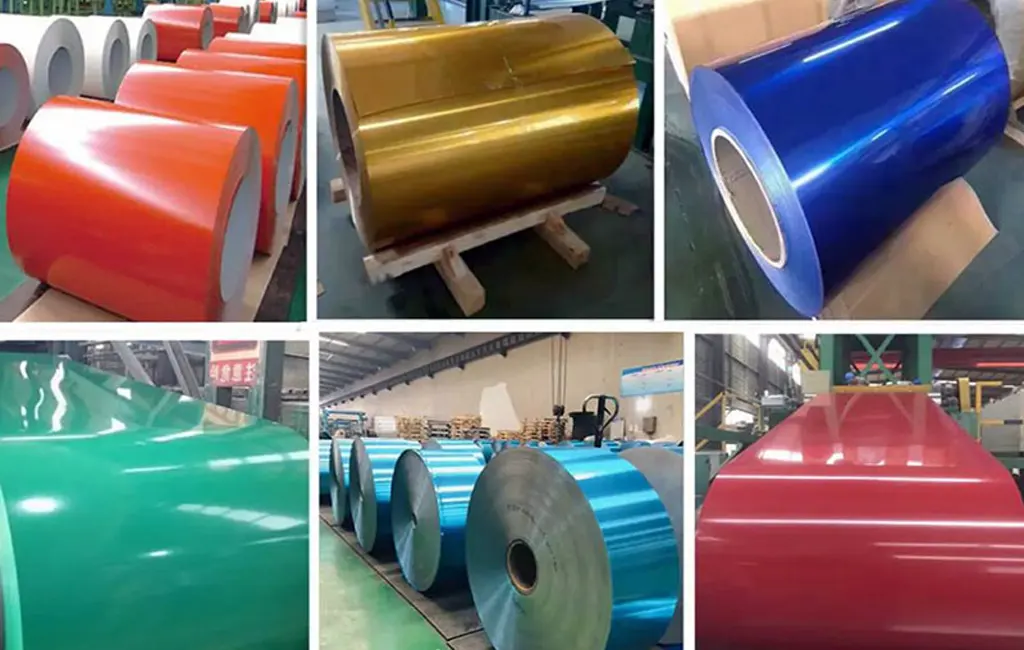
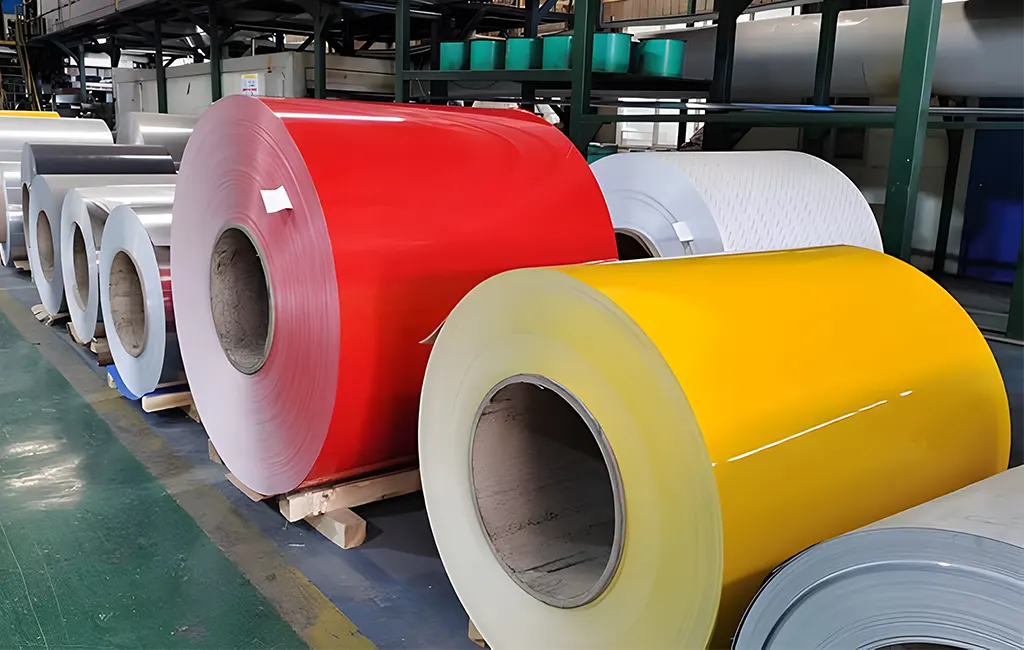
Inconsistent coating curing can negatively affect the flexibility, adhesion, and forming performance of color-coated aluminum coil, particularly during roll forming, folding, and bending operations. During coil coating production, the paint film must undergo controlled thermal curing to achieve the required crosslinking and mechanical properties [1]. Under-curing may result in insufficient film formation, poor adhesion, and reduced resistance to mechanical damage, while excessive curing can cause coating embrittlement and increase the risk of cracking during bending [2]. These problems are particularly important for aluminum coils used in roofing sheets, ceiling panels, curtain walls, and other applications involving repeated forming operations. Therefore, controlling the actual metal temperature and curing time is essential for maintaining consistent coating quality and bending performance.
1. How Does Inconsistent Curing Affect Coating Performance During Bending?
Coating curing determines how the resin system develops its final film properties. When curing conditions vary across a production run, different sections of the same aluminum coil may exhibit different mechanical behavior during subsequent fabrication.
| Curing Condition | Coating Characteristics | Potential Bending Problem | Quality Risk |
| Under-curing | Insufficient crosslinking | Poor adhesion and coating damage | Peeling or delamination |
| Excessive curing | Potentially excessive crosslinking or thermal degradation | Reduced coating flexibility | Surface cracking |
| Uneven curing | Inconsistent film properties | Different bending behavior across the coil | Inconsistent finished appearance |
| Proper curing | Stable film formation and balanced mechanical properties | Better coating integrity during forming | Reduced processing defects |
The actual effects depend on the resin chemistry, coating formulation, film thickness, and curing conditions. Excessive curing does not always cause embrittlement, but it can do so when the coating exceeds its specified processing window.
2. Why Is Metal Temperature More Important Than Oven Temperature?
One common quality-control issue in coil coating production is using oven temperature as the only indicator of curing performance.
In reality, Peak Metal Temperature (PMT) is a more meaningful parameter because it represents the maximum temperature reached by the aluminum substrate during the curing process.
Several factors influence PMT:
- Oven Temperature: Determines the thermal environment inside the curing oven.
- Line Speed: Higher production speeds generally reduce the time available for heating and curing.
- Aluminum Thickness: Different substrate thicknesses heat up at different rates.
- Coating Thickness: Primer and topcoat thickness can influence the thermal requirements of the coating system.
- Paint Chemistry: Different polyester, SMP, and PVDF-based systems have different curing requirements [3].
Manufacturers should follow the paint supplier’s specified PMT and curing-time window rather than applying one fixed temperature to every coating formulation.
3. Which Coating Properties Determine Bending Resistance?
Bending performance is influenced by both the aluminum substrate and the organic coating film. Even when the aluminum alloy has suitable formability, an unsuitable coating formulation or curing process can cause surface defects during fabrication.
Important properties include:
- Coating Flexibility: Determines the coating’s ability to accommodate deformation without cracking.
- Adhesion: Helps prevent the coating from separating from the aluminum substrate during bending [4].
- Hardness: Excessive hardness combined with insufficient flexibility may increase the risk of coating damage.
- Film Thickness: Excessive coating thickness can increase stress within the coating during tight-radius bending.
- Aluminum Alloy and Temper: Substrate elongation and mechanical properties influence the achievable bending radius.
For example, color-coated 3003 or 5052 aluminum coil may be selected for architectural forming applications, but the appropriate alloy and temper must be determined according to the required bending radius, sheet thickness, and forming process.
4. How Can Buyers Identify Curing-Related Bending Problems?
Buyers should evaluate coating performance through practical forming tests rather than relying exclusively on visual inspection or coating thickness measurements.
Recommended quality checks include:
| Test Method | Purpose | What to Observe |
| T-Bend Test (ASTM D4145) | Evaluate coating flexibility during bending | Cracking and coating damage |
| Cross-Cut Adhesion Test (ASTM D3359) | Evaluate coating adhesion [4] | Peeling or coating separation |
| Impact Resistance Test (ASTM D2794) | Evaluate resistance to deformation-related damage | Cracking or loss of adhesion |
| Film Thickness Test | Verify coating thickness | Compliance with specified DFT |
| PMT Monitoring | Verify curing conditions | Consistency with paint supplier requirements |
The T-bend test is particularly useful for evaluating prepainted metal coil [1]. The test result should be specified according to the coating system and application requirements. A 0T result, for example, should not be assumed achievable for every coating formulation or aluminum substrate.
5. How Can Manufacturers Prevent Inconsistent Curing and Coating Cracking?
Maintaining consistent curing conditions requires coordinated control of the coating formulation, production equipment, and aluminum substrate.
Manufacturers should implement the following measures:
- Monitor Peak Metal Temperature: Use calibrated temperature measurement systems to verify actual substrate temperature.
- Control Production Line Speed: Maintain a suitable heating and curing time for the selected coating system [2].
- Follow Paint Supplier Specifications: Use the recommended curing window for the specific resin formulation.
- Maintain Uniform Coating Thickness: Control primer and topcoat application across the coil width.
- Perform T-Bend Testing: Evaluate coating flexibility using representative production samples [1].
- Inspect Different Coil Positions: Check samples from the beginning, middle, and end of production to identify possible curing variations.
References
[1] Wikipedia contributors. Coil coating [EB/OL]. 2026-03-29.
[2] Wikipedia contributors. Curing (chemistry) [EB/OL]. 2026-03-29.
[3] Wikipedia contributors. Polyvinylidene fluoride [EB/OL]. 2026-03-29.
[4] Wikipedia contributors. Adhesion [EB/OL]. 2026-03-29.